
MOQ by Product Category: What Changes Across Glassware Types
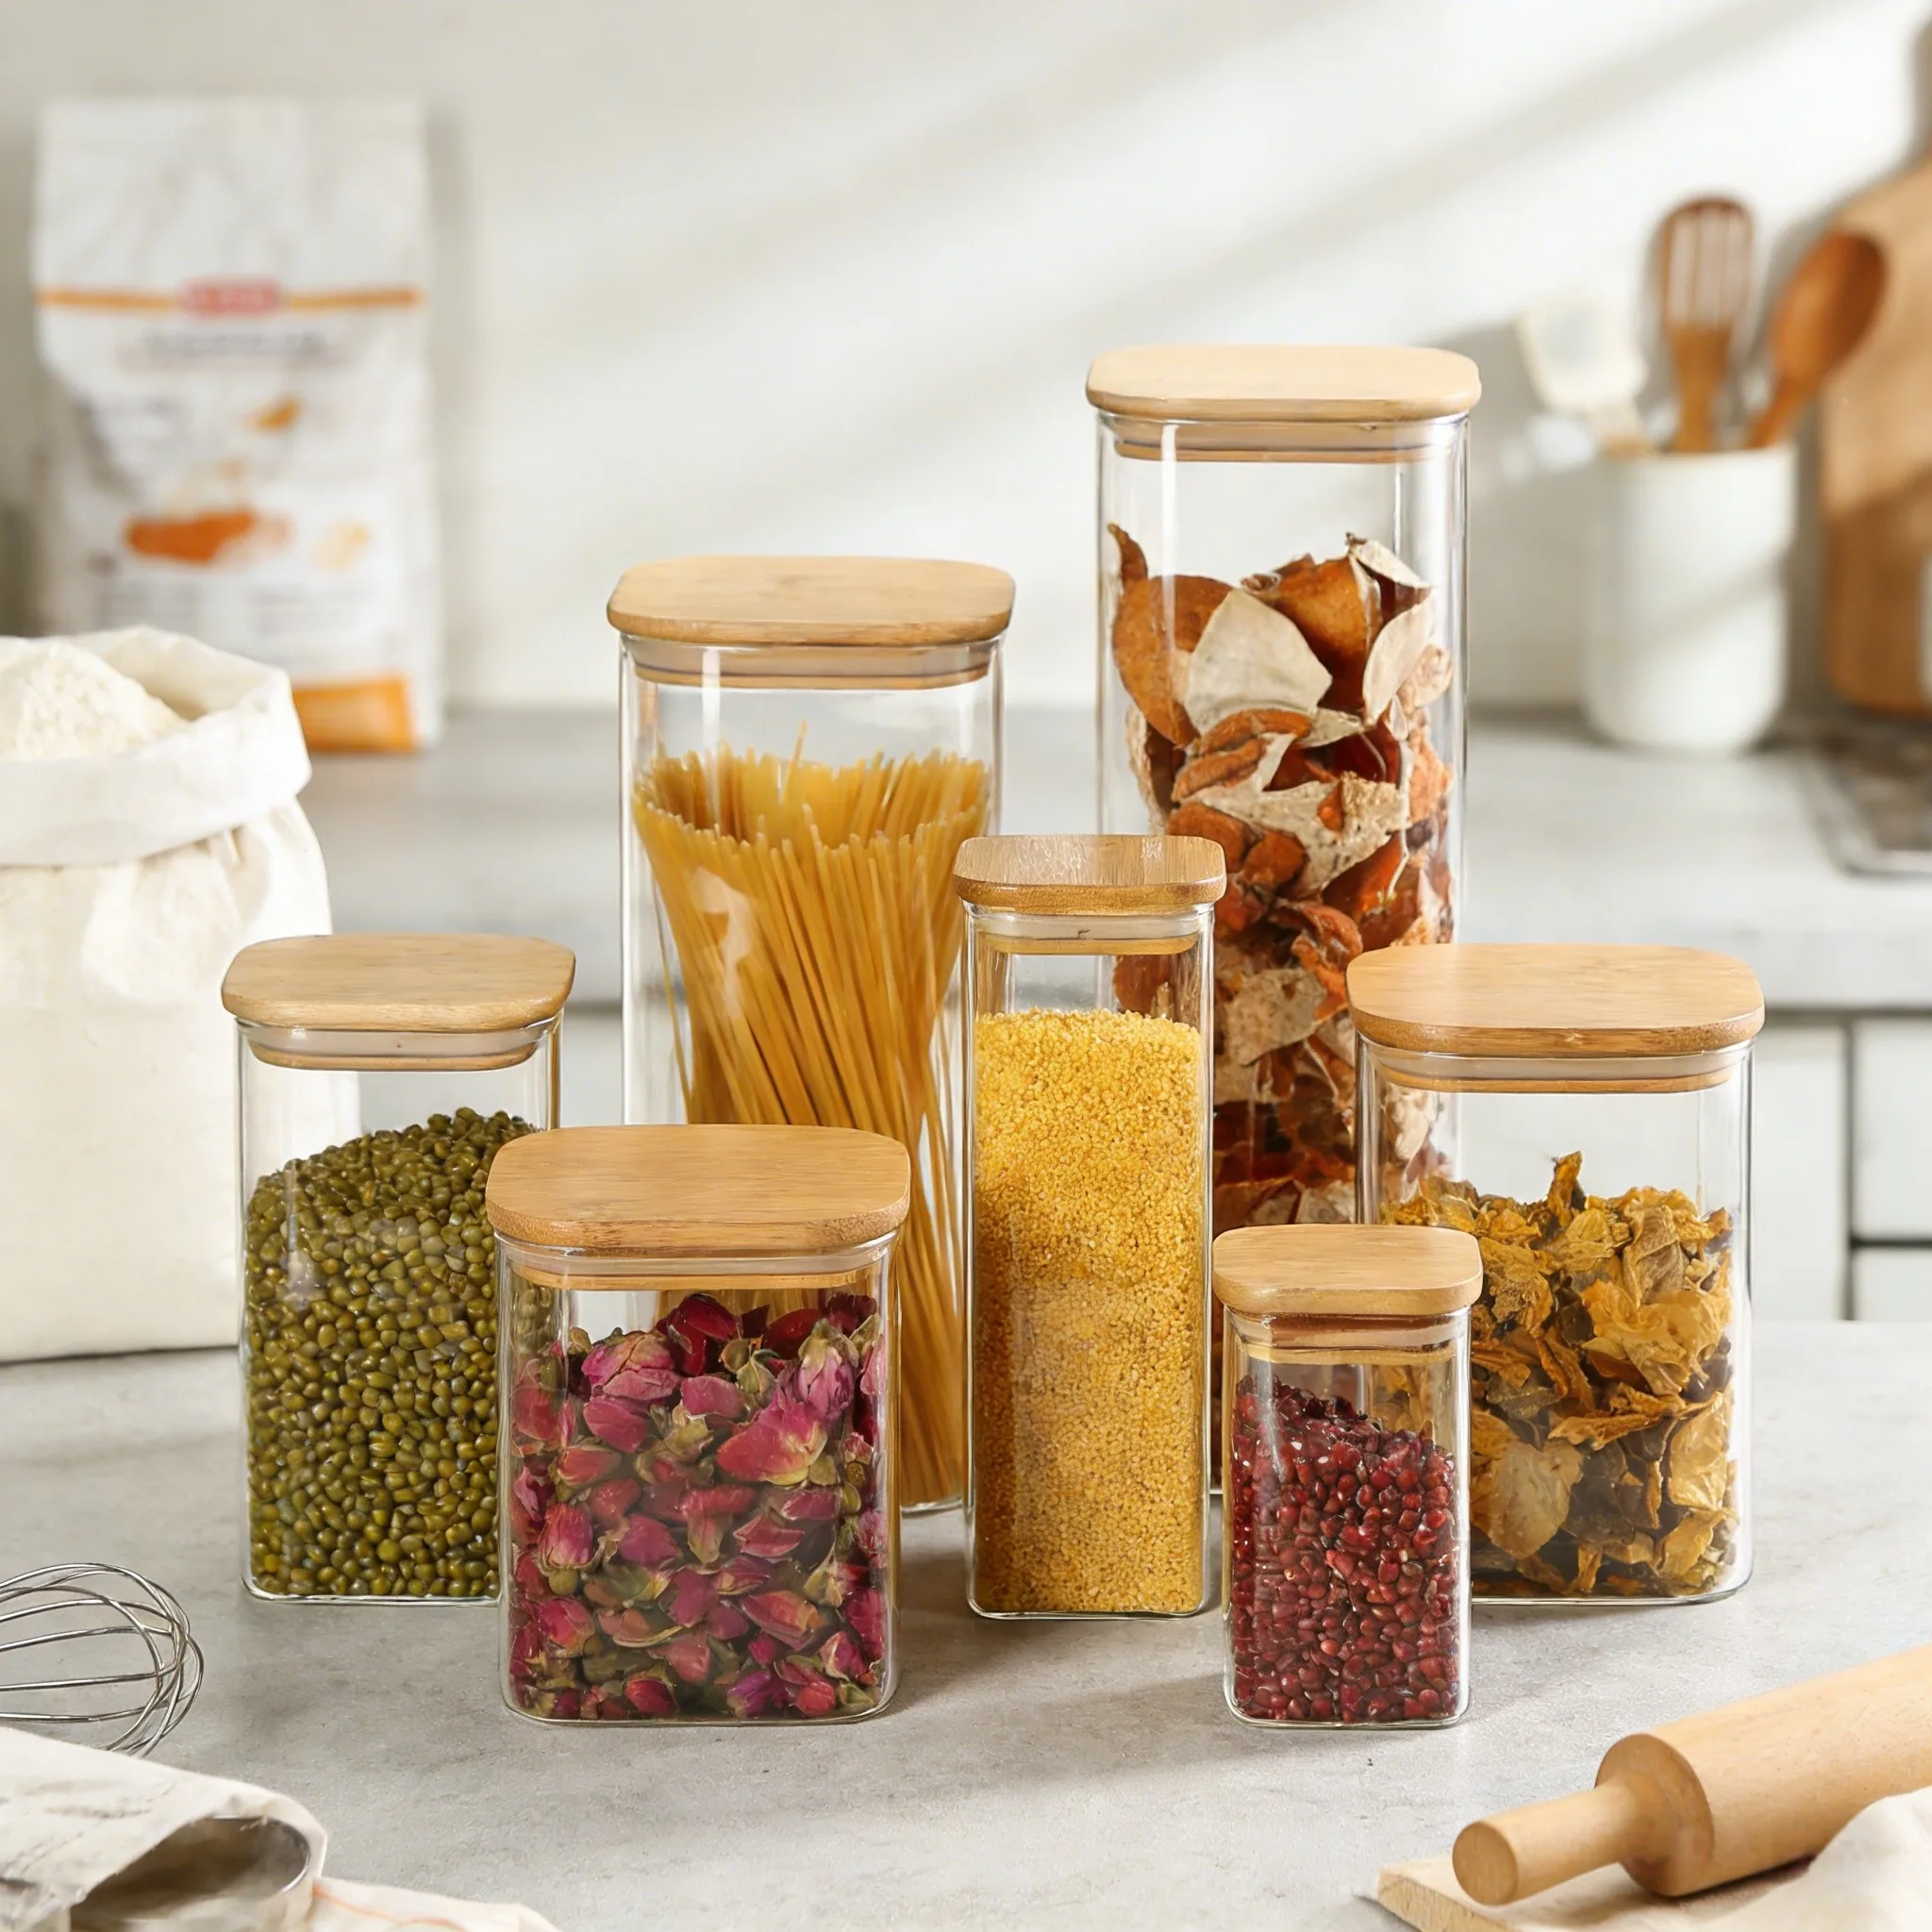
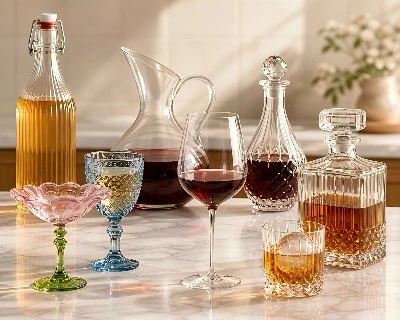
A buyer asks whether every category shares one minimum, and the honest answer is that the published minimum is the same number for everyone while the quantity that actually moves is not. What differs is how much risk a shape carries before it can be produced, and that risk is what a minimum is really pricing. A straight sided jar and a sculpted decanter may sit in the same quotation with the same headline figure, and they do not cost the same to make well.
Updated 22 October 2026 · MOQ 1000 pcs · 48 hours for a 3D sample · 7 to 10 business days for a physical sample
One number, different meanings
Before anything else, separate the two things that get called the minimum. One is the commercial floor the factory will not go below. The other is the quantity that makes a specific shape producible at an acceptable cost. The first is published. The second is what actually varies by category.
This distinction matters because a quotation usually shows the first and quietly assumes the second. When a buyer compares two suppliers at the same headline figure, they are comparing a stated floor rather than a producible quantity, and a great deal of the confusion in the first round of sourcing comes from that gap.
A minimum is not a promise that one shape costs the same as another. It is a promise that below a certain count the factory cannot spread the setup, the trial, and the inspection cost across enough units.
Where shape complexity actually comes from
Complexity is not a matter of taste or of price position. It comes from a small number of physical features, and each one creates a specific kind of production difficulty. Learning to name them is what lets a buyer predict the threshold before the quotation arrives.
Read that table as a set of questions rather than a list of penalties. A jar with a straight wall and a simple shoulder is easy. A decanter with a curved body and a narrow neck is difficult, and it is difficult for a reason that has nothing to do with how sophisticated the buyer wants it to look.
How geometry turns into production risk
A complex shape costs more to make, but the extra cost does not arrive as a higher unit rate. It arrives as risk, and risk is priced as a quantity. Understanding the three sources of that risk explains why the threshold moves.
A simple profile reaches a stable rhythm within a short run. A sculpted or asymmetric body needs the line to find its rhythm first, and the units produced during that settling are the ones most likely to be rejected. A factory cannot absorb a high reject rate on a small run and still make the numbers work, so the run has to be large enough to average the settling out.
Tooling for a simple straight sided form is robust. Tooling for an undercut, a deep curve, or a thin transition carries more risk of damage during cleaning and handling. The factory protects that risk by working with a longer run and by holding more of the same tooling in a stable state, rather than by changing it between small batches.
Each feature that varies along the body, the neck, or the joint is a point where a piece can be judged out of tolerance. A simple shape has one measurement band. A complex shape has several, and a run that must pass all of them is a run that has to be long enough for the judgment to be reliable rather than hurried.
The mechanism is straightforward: complexity creates a reject rate, a reject rate needs volume to average out, and volume is what the minimum is protecting. The minimum on a complex shape is the arithmetic of a run long enough to be predictable, and no amount of negotiation changes that arithmetic.
How risk becomes a higher threshold
When a factory quotes a higher minimum for a complex shape, the reason is one of three things, and they are worth separating because each one responds to a different buyer action.
None of those three reasons is fixed by negotiating. All three are fixed by reducing uncertainty before the run starts, and that work happens at the sample stage, not at the purchase order stage.
How to structure a first order
When a category carries a higher threshold, trying to get under the threshold is the wrong move. The useful question is how to make the first order small enough to learn from and large enough to be producible. Four steps do that.
Fix the shape before the quantity
A complex shape is the one thing you cannot change cheaply later. Agree the profile, the wall, the neck, and the joint against a physical sample first, and only then commit to a quantity. A 3D sample in 48 hours settles the visual question. A physical sample in 7 to 10 business days settles the question that matters, which is whether the shape behaves as intended under the tooling.
Treat the first run as a specification run
The purpose of a first order for a complex shape is to confirm that the line can produce it repeatably. That is worth paying for with a higher unit rate if it saves a failed production run later. It also means the first order should carry a specification you can hold the factory to, not a specification you intend to refine after the goods land.
Keep the program in one run
Every additional release adds a changeover, and a changeover is exactly the event that damages an aggressive cavity and restarts the settling. Consolidating a planned program into one larger run usually costs less than the equivalent quantity split across three small ones, because the risk is paid once instead of three times.
Plan the timing from the run, not the sample
A complex program does not move at the speed of a simple one. Production runs 30 to 60 days for a standard order, and a complex shape with a longer annealing and a wider inspection is better planned at the upper end of that window. Building the schedule from the sample date rather than the order date is what keeps a launch from arriving before the goods do.
Three assumptions that cost money
Most minimum disputes in this category are not about the number. They are about three beliefs that were never tested, usually because they felt obvious enough to skip.
It does not. A high minimum can be a sign of a complex program that genuinely needs volume, or a sign that the factory does not want small orders at all. The way to tell them apart is to ask what the minimum is protecting. If the answer names a specific production risk, it is arithmetic. If the answer is policy, it is negotiable.
A range quoted as one line hides the fact that its shapes are not equally producible. A category that mixes a straight sided storage format with a sculpted pouring format has two thresholds inside one line, and the buyer who treats it as one will discover the difference at the point where a shape is scheduled, which is too late.
For a complex shape it is frequently the wrong lever, because a smaller run raises the reject rate per unit and therefore the unit cost. Sometimes the cheaper path to a lower commitment is a simpler shape in the same category rather than a smaller quantity of the complicated one.
Choosing the profile you can produce
The table below is the working decision: it maps a shape feature to the practical consequence and to the move that keeps the program inside a comfortable commitment. It is a starting point for a conversation, not a rule.
A note on production resources. Our factory runs 16 lines, 12 automated and 4 hand blown, and the split matters for this decision. Automated lines carry standard profiles and predictable runs. Hand blown lines carry the irregular and the sculptural, and their output depends on furnace time rather than on a machine cycle, which is why a hand blown shape carries a different threshold and a different lead time from a machine made one of similar volume.
Five questions to ask before you commit
These five questions turn a category minimum into something you can schedule against. Ask them at the specification stage, before the order is placed, because every one of them is cheap to answer early and expensive to answer late.
Ask for the minimum against the shape, not against the category. A range quoted as one line may carry two different thresholds inside it.
An automated line and a hand blown line produce the same volume with different lead times and different thresholds. Knowing the route fixes the schedule.
A factory that answers this plainly is telling you the shape is understood. A factory that answers vaguely is telling you the shape is not.
Written bands agreed against the physical sample turn inspection into a measurement. Agreed later, they turn into an argument.
This is the question that prevents an expensive surprise. A split run means two changeovers, and on an aggressive cavity that is the risk being paid twice.
Frequently asked questions
How minimums differ between glassware categories, why complex shapes carry a higher threshold, and what to confirm before placing an order.
Q: Is the MOQ the same for every glassware category?
A: The published minimum is the same figure, but the quantity that a particular shape can be produced at economically is not. Categories differ in how much risk a shape carries before it can be produced reliably, and that risk is what a higher threshold is pricing. Ask for the minimum against your specific shape rather than against the category.
Q: Why do complex shapes carry a higher minimum?
A: Because complexity creates a reject rate. A sculpted or asymmetric body has to settle before the line reaches a stable rhythm, and the pieces produced during that settling are the ones most likely to be judged out of tolerance. A run long enough to average the settling out is what the minimum protects.
Q: Does a higher minimum mean the factory is better?
A: No. A higher minimum can be the arithmetic of a genuinely complex program, or it can be a policy decision not to take small orders. The way to tell is to ask what the minimum protects. A specific production risk means arithmetic. A general policy statement means negotiable.
Q: Is it better to order a smaller quantity of a complex shape or a simpler shape?
A: For a complex shape, a smaller run often makes the unit cost worse rather than better, because the reject rate is spread across fewer units. Choosing a simpler shape within the same category is frequently the cheaper way to reduce the commitment.
Q: What is the fastest way to reduce the minimum on a complex design?
A: Reduce the uncertainty before the run. Agree the profile against a physical sample, confirm the tolerance bands in writing, keep the program on one line and in one consolidated run, and then ask the factory to quote the minimum against that settled specification. That is a different question from asking for a lower number against a sketch.
Q: How does hand blown production affect the minimum and the lead time?
A: Hand blown output depends on furnace time rather than on a machine cycle, so it carries a different threshold and a different lead time from a machine made shape of similar volume. Our factory runs 16 lines, 12 automated and 4 hand blown, and the route chosen for a design determines the schedule. Ask which route will run your order.
Send the shape, not the number
The fastest way to get an accurate minimum is to describe the product itself, because the minimum follows the shape. Send a profile, a capacity, and a neck or closure requirement, and we will tell you which route will run it and what the minimum will be for that route.